
Views: 0 Author: Site Editor Publish Time: 2026-10-20 Origin: Site
A good blister package must do more than fit the product. It also has to form consistently, release from the mold, maintain enough wall thickness, provide a reliable sealing surface and run efficiently through trimming and downstream packaging operations.
That makes blister packaging design a manufacturing decision as much as a visual or structural one.
For thermoformed blister packaging, five areas deserve particular attention from the beginning: cavity depth, draft, flange geometry, venting and seal area. Material selection, sheet thickness and mold design then need to support those features as one system.
Before designing the cavity, define what the package actually needs to do.
Key questions include:
What are the product's maximum dimensions?
How much movement inside the cavity is acceptable?
Does the product need to be tightly retained or simply enclosed?
Is the package clear for retail display?
Will it be sealed to card, film or another material?
Is the product loaded manually or automatically?
Does the blister need a hang hole or other display feature?
What production volume is expected?
A cavity designed only around the product's CAD dimensions can create problems later. Clearance, draft, forming depth, trim tolerance and sealing space also have to be included.
For new projects, it is useful to review the package together with the forming tool. MINGDU's custom thermoforming mould solutions include forming and cutting-related tooling that can be developed around the intended product and production process.
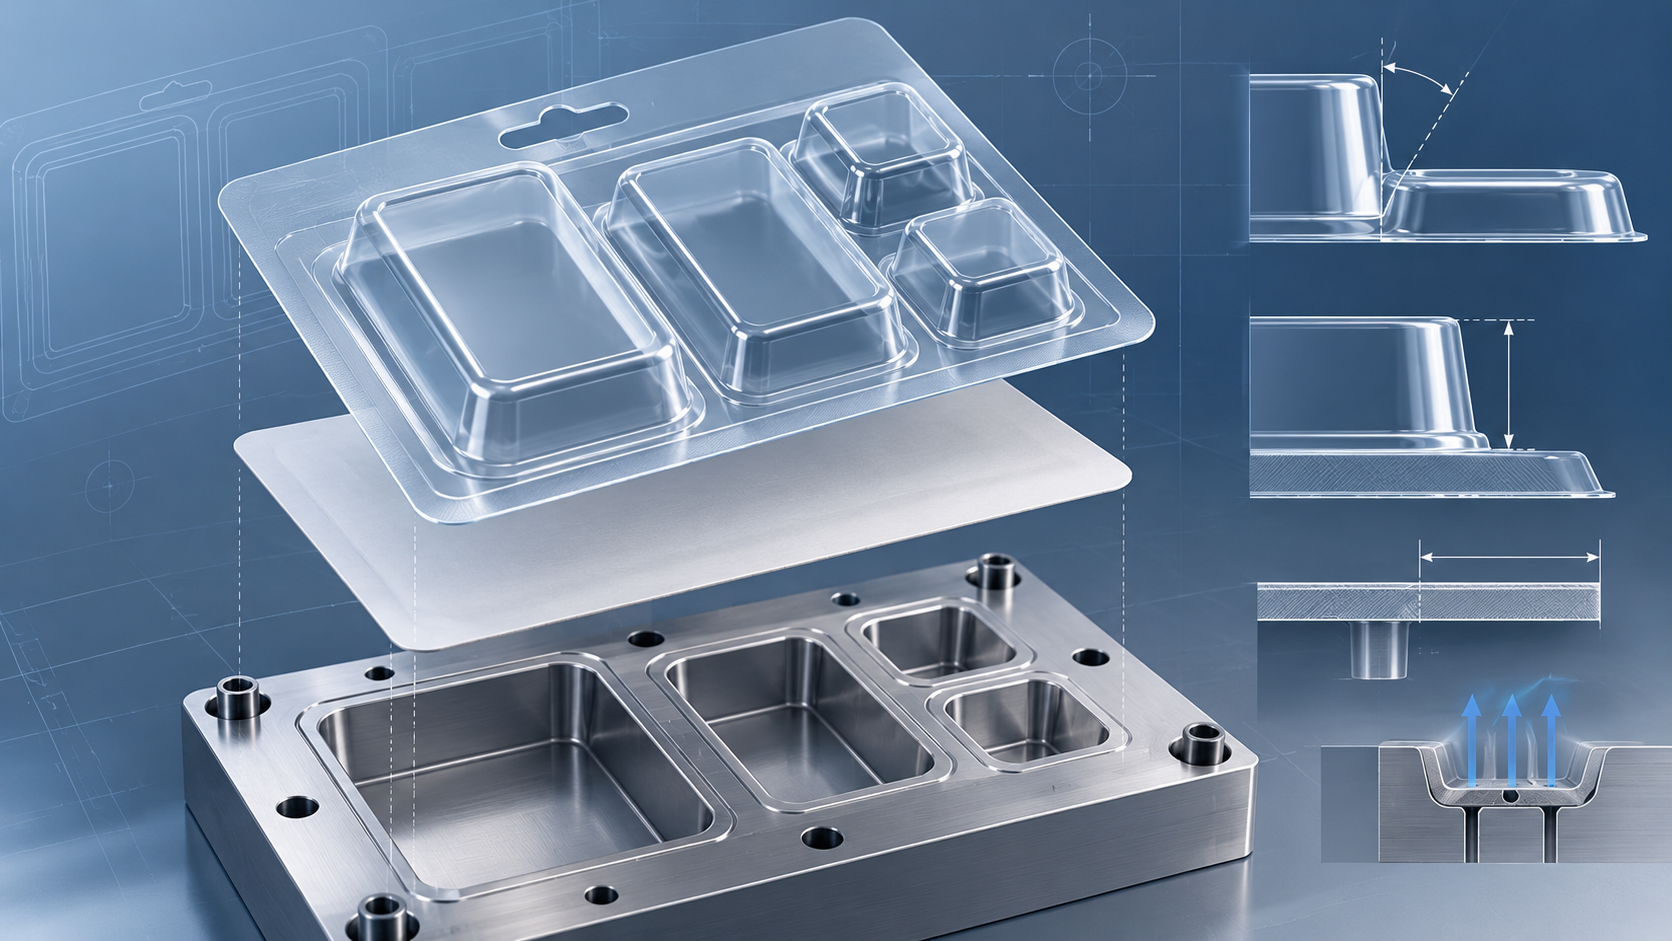
The cavity determines how the product sits in the package, but it also determines how far the heated sheet must stretch.
Important cavity dimensions include:
Length and width
Depth
Product clearance
Bottom radius
Sidewall angle
Local recesses
Retention features
The goal is usually to provide enough space for reliable loading while preventing unnecessary movement during handling.
An extremely close-fitting blister may look attractive in CAD but can make production and packing more difficult.
Possible problems include:
Product loading becomes difficult
Normal product tolerances cause interference
Forming shrinkage affects fit
Small dimensional changes create rejected packages
The cavity should therefore consider both product tolerance and thermoforming tolerance.
The opposite problem is an oversized cavity.
Too much clearance can allow the product to move, reduce presentation quality and increase the overall package size.
A good blister cavity balances:
product fit + manufacturing tolerance + protection + material efficiency
One of the most important relationships in thermoforming blister packaging is between cavity depth and sheet stretching.
When heated plastic is drawn into a cavity, the material does not remain at its original thickness. The deeper and more complex the cavity becomes, the more the sheet must stretch.
This can create thinner areas around:
Bottom corners
Deep sidewalls
Narrow cavities
Transitions between deep and shallow sections
A deeper blister is therefore not simply a taller version of a shallow blister.
Before finalizing the depth, consider:
Starting sheet thickness
Cavity width relative to depth
Corner radii
Material forming behavior
Heating uniformity
Whether pre-stretch or plug assist may be needed
Minimum acceptable finished wall thickness
If a design requires a very deep cavity with a small footprint, increasing the starting sheet thickness alone may not solve the problem. The cavity geometry may also need to change.
Draft is the slight angle added to walls that would otherwise be vertical.
Its purpose is straightforward: after forming and cooling, the blister needs to release from the mold without excessive resistance or distortion.
Zero draft may be possible in selected geometries, particularly with certain female features, but it gives the process less tolerance.
As a general design starting point, a small positive draft is safer than a perfectly vertical wall. Male features normally require more draft than female cavities because cooling plastic tends to shrink onto a male surface.
The final angle depends on:
Material
Mold type
Cavity depth
Surface finish
Shrinkage
Part geometry
Release method
For many designs, approximately 1–2° on suitable female features and 3° or more on male features can be used as an initial engineering discussion point—not as a universal specification.
Insufficient draft may lead to:
Difficult demolding
Distorted cavities
Surface scuffing
Longer release time
Irregular parts
Increased dependence on eject air
Draft should therefore be considered during the first design review, not added after the mold is already manufactured.
Sharp corners look precise on a drawing, but they are difficult locations for a heated plastic sheet.
As the material enters a tight corner, it must stretch rapidly over a small area.
Possible results include:
Local thinning
Weak corners
Poor mold definition
Inconsistent wall thickness
Stress concentration
Deeper cavities generally benefit from more generous radii.
This does not mean every blister needs visibly rounded geometry. The objective is to use enough radius to support material flow while still meeting the required package appearance and product fit.
A useful design principle is:
The deeper the draw, the more important it becomes to review radii, material distribution and heating together.
The flange is the flat area surrounding the blister cavity.
It may look simple, but it can perform several jobs:
Provide a sealing surface
Support trimming
Position the blister against a card
Improve package rigidity
Provide space between adjacent cavities
Support automated handling
A common mistake is to finish the cavity first and leave whatever area remains for the flange.
Instead, the flange should be designed at the same time as the cavity.
There is no single correct flange width for every blister package.
The required width depends on:
Sealing method
Backing material
Product size and weight
Trim process
Package layout
Sealing equipment
Required seal strength
Making the flange too narrow can leave insufficient room for reliable sealing or trimming.
Making it unnecessarily wide increases material usage and may reduce the number of cavities that fit within each forming cycle.
A wide flange is not useful if it is not sufficiently flat.
The seal area is the portion of the flange where the blister bonds to card, film or another lidding material.
For a stable seal, designers should consider:
Seal area width
Flange flatness
Material compatibility
Sealing coating
Temperature
Pressure
Dwell time
These variables work together.
A sealing defect cannot always be corrected by simply raising the temperature. If the flange is distorted or the plastic and lidding structure are incompatible, changing machine settings may not create a stable production process.
Raised features, cavity transitions or excessive distortion near the sealing zone can interfere with contact between the blister and backing material.
Whenever possible, maintain a clear and controlled sealing surface around the required package perimeter.
Thermoforming relies on the heated sheet reaching the mold surface.
As the plastic moves into the cavity, the air between the sheet and mold must escape.
This is the purpose of mold venting.
Vent locations are especially important around:
Deep cavity bottoms
Corners
Narrow details
Local recesses
Areas that tend to form last
Poor venting may cause:
Soft or incomplete details
Rounded corners where sharp definition was expected
Incomplete cavity depth
Inconsistent forming between cycles
However, simply adding large vent holes is not good practice either. Oversized or badly positioned vents may leave visible marks on the formed package.
Vent size, quantity and position should therefore be developed together with the actual thermoforming mould, material and forming conditions.
PET, PETG, PVC and PP can all be used for different thermoformed blister applications, but they do not behave identically.
| Material | Typical Design Consideration |
|---|---|
| PET / APET | High clarity and stiffness for many retail packages |
| PETG | Good clarity and useful formability for detailed cavities |
| PVC | Established forming and sealing performance in many traditional blister systems |
| PP | Useful where different thermal or chemical performance is needed |
Material selection should consider more than transparency.
Review:
Forming behavior
Stiffness
Impact requirements
Sheet thickness
Sealing compatibility
Product exposure
End-use temperature
Recycling requirements
Applicable regulatory requirements
For a broader material comparison, see the Thermoforming Materials Guide.
Blister designers should not specify a sheet thickness and assume that the entire formed package will retain that thickness.
The sheet stretches during forming.
That means the finished wall thickness depends on:
Draw depth
Cavity geometry
Sheet temperature
Material
Forming pressure or vacuum
Pre-stretching
Plug assist
Mold design
The critical measurement is therefore often the minimum thickness at important locations, not simply the nominal starting gauge.
When evaluating prototypes, measure areas such as:
Bottom corners
Deep cavity walls
Retention features
Narrow transitions
Areas close to the trim line
A blister is not finished when it leaves the forming cavity.
It still needs to be separated from the surrounding web.
The package design should therefore include:
Trim line
Cutting clearance
Cavity spacing
Registration requirements
Scrap web
Nesting efficiency
Poor cavity layout can increase material waste even if each individual blister forms correctly.
For high-volume packaging, the objective is to achieve a practical balance between:
part quality + cavity count + material utilization + cutting reliability
MINGDU's Thin-Gauge Thermoforming Machines are designed for thin plastic packaging applications such as blister packs, trays and clamshells, making forming area, tooling layout and downstream cutting important parts of equipment selection.
Before releasing a blister design for tooling, review the following:
| Design Area | Questions to Check |
|---|---|
| Product fit | Is there enough tolerance for loading and product variation? |
| Cavity depth | Can the sheet reach the required depth without excessive thinning? |
| Draft | Can the formed blister release reliably from the mold? |
| Corner radius | Are deep corners causing unnecessary stretching? |
| Flange | Is there sufficient space for sealing and trimming? |
| Seal area | Is the sealing surface flat, clear and compatible with the backing? |
| Venting | Can trapped air escape from deep and detailed areas? |
| Material | Does the plastic meet clarity, stiffness, forming and sealing requirements? |
| Thickness | Is the minimum finished wall thickness acceptable? |
| Trim layout | Can parts be cut efficiently without excessive scrap? |
Check:
Heating
Vacuum or pressure
Venting
Cavity depth
Material temperature
Review:
Draw depth
Corner radius
Sheet thickness
Heating distribution
Pre-stretch or plug assist
Review:
Draft
Shrinkage
Male features
Surface texture
Release method
Check:
Flange flatness
Seal area width
Material compatibility
Coating
Sealing temperature
Pressure and dwell time
Review:
Cavity spacing
Flange width
Nesting
Sheet width
Trim layout
Do not reduce material simply by making the sheet thinner. First determine where material is being consumed and whether the finished package still meets strength and forming requirements.
A reliable blister package is the result of several decisions working together:
Product → Cavity → Material → Draft → Flange → Venting → Mold → Forming → Sealing → Trimming
Problems occur when these decisions are treated separately.
A cavity may be visually correct but difficult to form. A blister may form perfectly but have an unreliable sealing flange. A package may pass prototype testing but waste excessive sheet material when arranged in a production mold.
For this reason, blister packaging design should be reviewed with both tooling and production in mind.
MINGDU provides custom forming and cutting mould solutions and Thin-Gauge Thermoforming Machines for plastic packaging production. For a new blister project, the most useful starting information includes the product drawing, proposed material, sheet thickness, cavity depth, package layout and target production output.
There is no single factor. Product fit, cavity depth, draft, material distribution, flange design, venting and sealing must work together.
The required draft depends on mold type, material, depth, surface and shrinkage. Small positive draft is generally preferable to zero draft, and male features typically require more draft than female cavities.
The flange can provide the sealing, trimming and handling area around the cavity. Poor flange geometry can cause sealing problems, material waste or difficult trimming.
Vents allow trapped air to leave as the heated sheet approaches the mold surface. Good vent placement helps reproduce deep corners and detailed cavity features.
Sometimes, but not automatically. Deep forming increases stretching, so starting gauge may need to increase, but cavity geometry, corner radii, material, heating and forming method should also be reviewed.
PET, PETG, PVC and PP can all be suitable depending on the application. Material should be selected according to forming behavior, clarity, stiffness, sealing, end-use conditions and packaging requirements.
Successful blister packaging design is not about maximizing cavity depth or minimizing material at all costs. It is about creating a package that can be formed, released, sealed and trimmed consistently.
The most important design questions are practical:
Can the material reach the bottom of the cavity without excessive thinning?
Is there enough draft for reliable release?
Is the flange wide and flat enough for sealing?
Can trapped air escape through properly designed vents?
Does the selected material work with the forming and sealing process?
Answering those questions before tooling is manufactured reduces trial-and-error later and creates a stronger foundation for stable high-volume thermoforming production.


